
Disclosure: As an Amazon Associate, we earn from qualifying purchases. If you click a link on this page and make a purchase, we may receive a small commission at no extra cost to you.
Choosing the wrong stick welding rod can leave you with poor weld quality, hard-to-control slag, or joints that crack after cooling. The ARCCAPTAIN E7018 3/32-inch welding rod offers a low-hydrogen coating, a 70,000 PSI tensile-strength classification, and support for AC or DC-positive welding. Its smaller diameter can help you control the weld puddle, but correct storage and clean steel are essential. This review explains its confirmed specifications, practical uses, limitations, and whether the 5 lb package is right for your projects.
Quick Verdict
Rating: Recommended with caveats
Best For: Fabricators, equipment repair shops, and experienced DIY welders who need low-hydrogen electrodes for clean carbon steel.
Bottom Line: The ARCCAPTAIN E7018 combines a manageable 3/32-inch diameter with a low-hydrogen, iron-powder coating designed for smooth welding and good puddle control. It is worth considering for prepared steel joints, but moisture-sensitive storage and the need for correct welding procedures make it less convenient than general-purpose rods.
ARCCAPTAIN E7018 Welding Rod Specifications
| Specification | Detail |
|---|---|
| Brand | ARCCAPTAIN |
| Model / Part Number | E7018-3/32-5LB |
| Product Type | Stick welding electrode for SMAW |
| Electrode Classification | AWS E7018 |
| Electrode Diameter | 3/32 inch (approximately 2.4 mm) |
| Electrode Length | 14 inches (approximately 356 mm) |
| Package Quantity | 5 lb package of electrodes |
| Listed Item Weight | 5.28 lb |
| Package Dimensions | 14.09 × 3.11 × 1.42 inches |
| Flux Coating | Low-hydrogen, iron-powder type |
| Tensile-Strength Classification | 70,000 PSI minimum for AWS E7018 deposited weld metal under specified test conditions |
| Operating Current | AC or DCEP (DC electrode positive) |
| Amperage Guidance | Approximately 70–110 A is a general reference range for comparable 3/32-inch E7018 rods. Confirm settings using the product instructions. |
| Welding Positions | Flat, horizontal, vertical-up, and overhead; not normally used for vertical-down welding |
| Compatible Materials | Carbon steel and suitable low-alloy steels; higher-carbon applications require procedure review |
| Storage Requirement | Protect the low-hydrogen coating from moisture and follow the applicable storage instructions |
| Amazon ASIN | B0D9QDZB5R |
Specification note: The model, size, weight, and package dimensions are based on published ARCCAPTAIN product information. The amperage guidance is based on general E7018 technical references, not a confirmed ARCCAPTAIN-specific operating chart. Actual results depend on your machine, joint design, material, and technique.
What Is the ARCCAPTAIN E7018 Welding Rod?
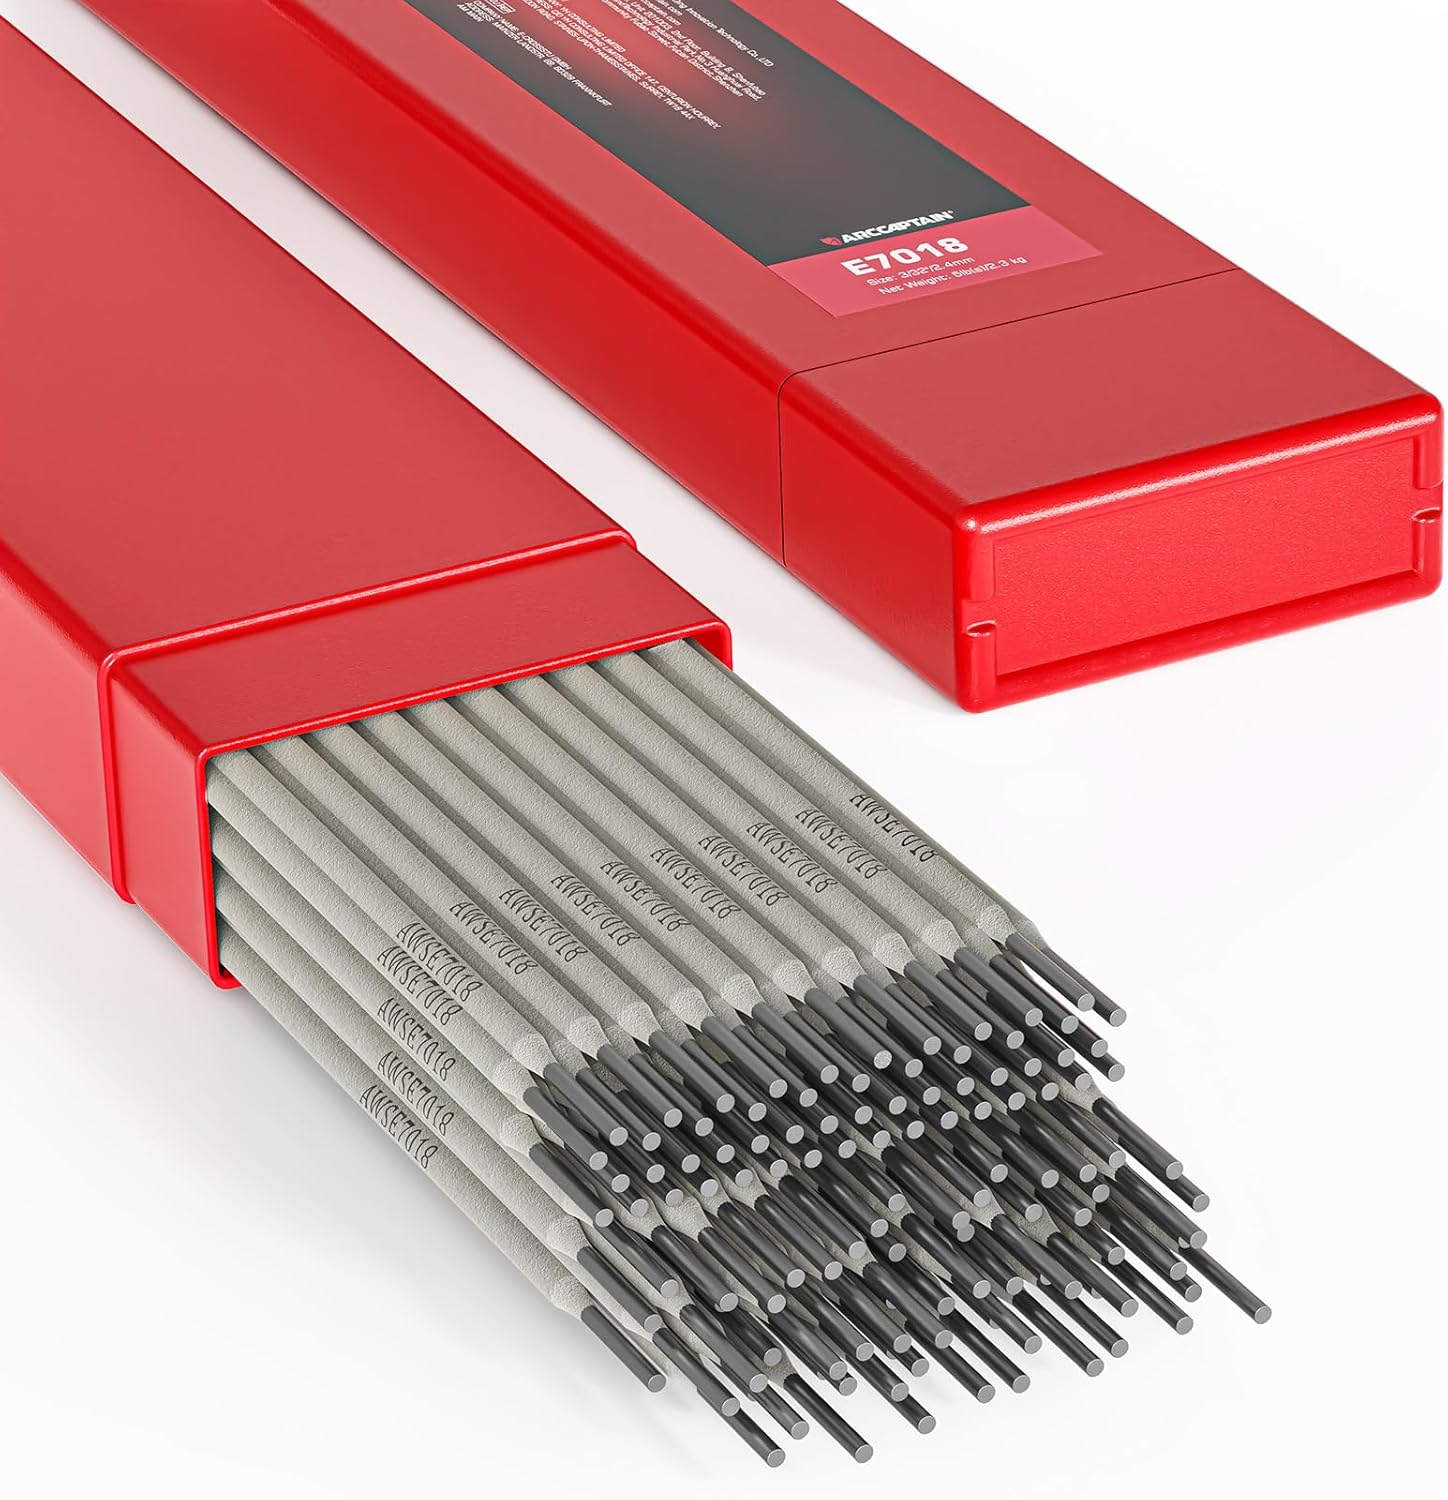
The ARCCAPTAIN E7018 is a covered welding electrode designed for shielded metal arc welding (SMAW), commonly called stick welding. This version has a 3/32-inch core diameter, a 14-inch length, and a 5 lb package. It uses the E7018 low-hydrogen, iron-powder electrode design.
The E7018 classification identifies an electrode type intended for welds that need good mechanical properties and reduced hydrogen-related cracking risk. The iron powder in its coating can support efficient metal deposition, while its slag system helps protect the molten weld during solidification.
ARCCAPTAIN markets these electrodes for steel frames, heavy equipment, pipelines, bridges, and related fabrication. These are potential applications, not automatic approvals for critical work. If your project involves a load-bearing structure or pressure system, you must verify the filler metal and welding procedure against the applicable requirements.
What Makes the 3/32-Inch Size Useful?
A 3/32-inch electrode is smaller than a 1/8-inch rod. It generally needs less current and deposits less metal per unit of travel. That can make it easier to manage the puddle on smaller joints, repair sections, and welds that require careful movement.
The tradeoff is productivity. A larger electrode may fill a wide groove faster when the machine and joint allow it. If you weld heavy plate throughout the day, compare the 3/32-inch package with ARCCAPTAIN’s available 1/8-inch E7018 version before ordering.
Who Should Buy It?
Best For
- Steel fabricators who use E7018 electrodes for properly prepared joints and controlled welding procedures.
- Equipment repair shops that need smaller-diameter, low-hydrogen stick electrodes for suitable carbon steel repairs.
- Experienced hobby welders with an AC or DCEP-capable machine and a reliable method for keeping electrodes dry.
Skip If
- You mainly weld thin sheet metal where burn-through is a concern and a lower-heat process may be better.
- You need to weld through heavy rust, paint, or dirt without properly preparing the steel.
- You cannot maintain the electrode storage conditions required for your work, especially on code-controlled projects.
Key Performance Features
Arc Stability and Spatter Control
ARCCAPTAIN describes its E7018 electrode as producing a stable arc with limited spatter. This fits the general behavior of well-handled E7018 electrodes, which are known for a relatively smooth arc and controlled metal transfer.
For you, a steady arc can make it easier to maintain a uniform bead while welding clean steel. Less spatter may also reduce the time spent cleaning nearby surfaces. However, incorrect amperage, poor electrode condition, or an excessively long arc can still create spatter and defects.
Do not assume the rod will strike perfectly every time. E7018 electrodes can be harder to restart after partial use because cooled flux and slag can cover the exposed core at the tip.
Low-Hydrogen Coating and Crack Resistance
The main reason to choose E7018 is its low-hydrogen design. Hydrogen can contribute to delayed cracking in susceptible steel welds, particularly when joint restraint, material composition, and cooling conditions increase the risk.
The electrode coating helps limit hydrogen entering the weld when the rods have been handled and stored correctly. This makes E7018 a common choice for applications where weld integrity matters more than the ability to burn through surface contamination.
There is an important limit. Low-hydrogen chemistry does not make a weld crack-proof. You still need suitable base metal preparation, correct heat input, proper joint design, and any required preheat or post-weld controls.
Iron-Powder Coating and Deposition
The iron powder in an E7018 coating contributes metal to the weld deposit. This is one reason E7018 is useful for filling grooves and making fillet welds in structural steel fabrication.
The 3/32-inch diameter provides a smaller puddle than a larger electrode under comparable conditions. It is a practical choice when control matters more than maximum deposition speed.
The slag system can produce a smooth-looking bead when your technique is correct. Still, slag removal is not always effortless. Joint shape, current, travel speed, and welding position can affect how easily it releases.
All-Position Welding Capability
ARCCAPTAIN lists this E7018 electrode as suitable for all-position welding. In practical terms, the E7018 classification supports flat, horizontal, vertical-up, and overhead work, but not normal vertical-down progression.
Flat welding is generally the easiest place to establish consistent puddle control. Vertical-up and overhead welding take more practice because gravity changes how the molten metal and slag behave.
If most of your welding is overhead, the smaller 3/32-inch rod may be easier to manage than a larger electrode. You must still adjust current and travel technique for the position.
Package Size and Storage
This ARCCAPTAIN version contains 5 lb of electrodes. The published model number is E7018-3/32-5LB, and the listed package dimensions are 14.09 × 3.11 × 1.42 inches.
A 5 lb pack can be more practical than a larger package when you weld only occasionally. It lets you buy a smaller amount of consumable material, but the rods are still moisture-sensitive after their protective packaging is opened.
Do not assume a basic plastic container restores a moisture-exposed electrode to low-hydrogen condition. Storage and reconditioning need to follow the electrode manufacturer’s instructions and your applicable welding procedure.
Before You Buy: E7018 electrodes are sensitive to moisture. A sealed storage tube is useful for protection, but it may not satisfy the heated storage requirements of critical welding work. Also, storing rods at a holding temperature is not the same as properly rebaking moisture-exposed rods. Never use a universal 250°F rebaking rule. Check the electrode manufacturer’s instructions, exposure limits, and any applicable welding code before use.
How It Performs in Real Use
The following examples explain how this electrode is suited to common welding situations. They are application-based assessments, not results from independently documented hands-on tests of this specific ARCCAPTAIN package.
1. Structural Steel and Frame Fabrication
For prepared steel frames, angle iron, and suitable tubing, the E7018 classification offers a useful combination of weld strength and low-hydrogen characteristics. The 3/32-inch diameter can help you control a smaller weld pool around corners and fitted joints.
On thicker sections, you may need multiple passes to fill the joint correctly. Simply increasing the current is not a substitute for proper joint preparation, penetration, and a suitable welding procedure.
For structural work governed by a code, confirm the approved electrode classification, welding procedure specification (WPS), and welder qualifications before starting.
2. Heavy Equipment and Workshop Repairs
The 5 lb package is a reasonable format for repair shops that do not need a large stock of one electrode size. E7018 can be useful for suitable carbon steel brackets, equipment frames, and other prepared repair joints.
Before welding, identify the base metal. Some machine parts use hardenable or alloy steels that need special filler metals, preheat, or repair procedures. E7018 should not be treated as a universal solution for every damaged steel component.
If you work outdoors, protect the rods from rain, damp surfaces, and prolonged exposure to humid air.
3. Pipe and Pressure-System Fabrication
ARCCAPTAIN lists pipeline and pressure-related fabrication among the intended uses of its E7018 electrodes. In qualified procedures, E7018 may be used for fill or cap passes where the joint design and welding specification permit it.
The coating and puddle characteristics can suit controlled welding on prepared steel. However, a rod’s marketing description does not establish that a completed weld will pass radiographic inspection.
Pressure-system welding must follow the appropriate code, qualified procedure, and inspection requirements. Do not use this electrode for a pressure repair based on its E7018 designation alone.
4. Vertical-Up and Overhead Welding
The 3/32-inch electrode gives you a smaller amount of molten metal to manage compared with larger rod sizes. That can help on tight joints or overhead welds where puddle size matters.
For vertical-up work, use the travel pattern and current required by your procedure. Keep the puddle small enough to control, and avoid a wide weave that traps slag along the edges.
Overhead welds also need careful body position and full protection from falling sparks and slag. Practice on scrap steel before attempting a finished joint.
Pro Tip: E7018 generally works best with a short, controlled arc. In flat and horizontal welding, keep the electrode close to the puddle and use a steady drag technique. A long arc can increase spatter and make it harder to maintain good shielding. Adjust your angle for the joint and welding position.
Operating Guidelines and Best Practices
Good welding results depend on more than the electrode you buy. You need the right machine settings, clean base metal, suitable joint preparation, and correct technique.
Choosing the Right Amperage
Published guidance for comparable 3/32-inch E7018 electrodes commonly falls around 70–110 amps, depending on the specific electrode and welding position. Hobart Brothers gives approximately 80–100 amps as a general reference for this diameter.
That range is not a verified ARCCAPTAIN-specific setting. Begin with the electrode package instructions and your machine’s recommendations. For noncritical practice work, use suitable scrap material to fine-tune your arc and bead shape.
AC Versus DCEP Welding
ARCCAPTAIN states that this E7018 electrode can operate with AC or DC electrode positive, also called DCEP or DC reverse polarity.
DCEP is a common choice for E7018 welding. AC can also be useful when you have a compatible transformer or inverter machine. Actual arc-starting behavior depends on the equipment, including its open-circuit voltage and arc-control characteristics.
If you use a compact 120V stick welder, check its actual welding output and electrode compatibility. The input voltage alone does not tell you whether the machine can run E7018 reliably.
Preparing the Joint
- Remove contamination: Clean paint, oil, grease, heavy rust, and loose mill scale from the weld area.
- Check fit-up: Make sure the joint gap, bevel, and alignment suit the material thickness and required weld.
- Control the arc: Keep a short, stable arc and avoid excessive travel speed.
- Remove slag: Clean slag fully between passes before adding another weld bead.
- Finish the crater: Follow the correct procedure for filling the end crater to reduce the risk of defects.
Starting and Restarting the Rod
An unused E7018 rod may strike more easily than a partially burned rod. After welding stops, the flux can leave a hard, nonconductive coating over the electrode tip.
When restarting, remove the slag cap from the tip using an appropriate method, then establish the arc on the prepared joint. Avoid damaging the remaining flux coating, since broken coating can affect the weld.
Preheat and Heat Control
Some thicker, higher-carbon, or highly restrained steel joints need preheat to reduce cracking risk. The required temperature depends on material composition, thickness, joint restraint, hydrogen control, and the applicable welding procedure.
Do not apply one fixed preheat temperature to every E7018 welding job. Follow a qualified WPS or obtain guidance from a welding professional for critical or unfamiliar materials.
Electrode Storage and Moisture Control
Moisture control is one of the biggest practical differences between E7018 and many general-purpose stick electrodes. A low-hydrogen coating must remain in the condition required for the intended welding application.
Before Opening the Package
Keep unopened electrodes in their original packaging in a dry storage area. Inspect the package for damage or signs of moisture before use.
Do not assume that every retail package is hermetically sealed. Check the packaging and product instructions to understand how the rods were supplied.
After Opening the Package
For casual, noncritical fabrication, a suitable dry storage container can help limit exposure. For critical low-hydrogen welding, applicable procedures may require an electrode holding oven with a controlled temperature.
Exposure limits vary according to the electrode type and governing specifications. The original article’s fixed four-hour rule should not be treated as a universal requirement for every E7018 product.
Can Moisture-Exposed Electrodes Be Reconditioned?
Some low-hydrogen electrodes can be reconditioned through a controlled drying process. However, correct temperatures and holding times vary with electrode type, coating condition, and manufacturer instructions.
Rebaking may require a much higher temperature than normal heated storage. The specific schedule must be confirmed before attempting reconditioning.
Do not use a kitchen oven intended for food preparation. Discard electrodes when the manufacturer requires it, especially if their coating is damaged or the rods have been exposed to conditions that cannot be corrected safely.
Safety Guidelines and Protective Gear
Stick welding exposes you to ultraviolet radiation, hot metal, electrical hazards, sparks, and welding fumes. Use a welding helmet with an appropriate filter shade for your current and process, along with safety glasses, flame-resistant clothing, suitable welding gloves, and protective footwear.
Keep combustible materials away from the welding area. Make sure your workpiece is stable and that cables, the electrode holder, and electrical connections are in good condition.
Use effective local fume extraction or other appropriate ventilation. Welding fumes can contain hazardous metal compounds and substances from electrode coatings and surface contaminants. Follow the product’s safety data sheet and applicable workplace exposure requirements.
Avoid welding coated, galvanized, or unknown materials without identifying the hazards and using appropriate controls. Never weld closed containers, tanks, or pressure vessels without the required professional procedures and safety precautions.
For load-bearing structures, lifting equipment, pressure components, or other safety-critical assemblies, use qualified welding personnel and follow the governing code.
Pros and Cons
Pros
- Low-hydrogen E7018 design is suited to applications where hydrogen-related cracking is a concern.
- 3/32-inch diameter offers a manageable electrode size for smaller prepared joints.
- Supports AC and DCEP welding power sources.
- Iron-powder coating is designed for steady deposition, a smooth arc, and limited spatter.
- 5 lb package is a practical quantity for smaller fabrication jobs and shops with modest usage.
Cons
- Low-hydrogen coating requires moisture control and may need heated storage for critical work.
- Not a good choice for welding directly through heavy paint, rust, oil, or other contamination.
- Smaller diameter deposits less metal per pass than larger electrodes and can require more passes on thick joints.
Check Current Price on Amazon →
Is It Worth the Price?
The ARCCAPTAIN E7018 3/32-inch 5 lb package is worth considering if you specifically need low-hydrogen stick electrodes for prepared steel. Its useful features are the E7018 classification, AC/DCEP compatibility, and smaller electrode diameter. These matter more than cosmetic packaging or promotional claims.
For occasional workshop use, the 5 lb quantity may be more convenient than buying a larger box. If you regularly weld heavy joints, a larger electrode size or package may be more economical, depending on current prices and your welding procedures.
The main extra cost is not always the electrode itself. Proper low-hydrogen storage may require heated equipment, especially for regulated welding work. Compare the total cost of the rods and the storage method before deciding that E7018 is the best value for your project.
How It Compares to Alternatives
ARCCAPTAIN E7018 vs E6010 and E6011: E6010 and E6011 are cellulosic electrodes often used for demanding root passes and situations where a more forceful, digging arc is useful. E6011 can operate on AC or DCEP, while conventional E6010 is generally used with DCEP. E7018 is a better match when your procedure calls for a low-hydrogen electrode on properly prepared steel. It is not a direct substitute for a specified E6010 or E6011 root pass.
ARCCAPTAIN E7018 vs E6013: E6013 is commonly used for general fabrication and lighter-gauge work. It can be convenient for hobby welding where low-hydrogen properties are not required. E7018 makes more sense when a suitable procedure calls for its mechanical properties and hydrogen control. If you want E7018 but need faster filling on larger joints, compare ARCCAPTAIN’s 1/8-inch version with this 3/32-inch package.
Frequently Asked Questions
Can I use ARCCAPTAIN E7018 3/32-inch rods with a 120V stick welder?
Possibly. Your welder must provide enough output current and suitable arc-starting performance for E7018 electrodes. Check the machine’s supported electrode types and operating range rather than relying only on its 120V input rating.
What amperage should I use for 3/32-inch E7018 rods?
Comparable 3/32-inch E7018 electrodes commonly use settings around 70–110 amps, with approximately 80–100 amps often given as a general starting range. This is not a verified ARCCAPTAIN-specific recommendation. Follow the package guidance and adjust for your joint, welding position, and machine.
Does this ARCCAPTAIN E7018 electrode work on AC and DC welders?
Yes. ARCCAPTAIN identifies AC and DCEP as supported operating modes. Make sure your machine is compatible with E7018 electrodes and can provide suitable current and arc-starting characteristics.
How should I store ARCCAPTAIN E7018 rods after opening the package?
Protect opened rods from atmospheric moisture and follow the manufacturer’s storage instructions. Critical low-hydrogen welding may require controlled heated storage and specific exposure limits. A simple airtight container is not always enough to satisfy those requirements.
Can moisture-exposed E7018 rods be dried and reused?
Some low-hydrogen electrodes can be reconditioned, but the correct procedure depends on their coating and exposure history. Never assume a low-temperature holding oven will restore moisture-damaged rods. Follow the electrode manufacturer’s approved reconditioning instructions and discard unsuitable electrodes.
Can I weld rusty or painted steel with E7018 electrodes?
E7018 works best on properly cleaned steel. Remove paint, oil, heavy rust, and other contamination before welding. Leaving these materials on the joint can increase the risk of porosity, slag inclusions, and inconsistent weld quality.
Can I weld vertically or overhead with these 3/32-inch rods?
Yes. The E7018 classification supports flat, horizontal, vertical-up, and overhead welding. Vertical-down welding is not a normal application for this electrode. Use suitable current and technique for each position, and practice before making important joints.
Are ARCCAPTAIN E7018 rods suitable for structural or pressure welds?
ARCCAPTAIN markets E7018 for structural steel and pressure-related applications, but suitability depends on the specific project. Critical welds may require verified consumable certifications, a qualified welding procedure, trained personnel, and inspection. The electrode designation alone does not guarantee code compliance or X-ray inspection results.
The Bottom Line
The ARCCAPTAIN E7018 3/32-inch welding rod is worth considering if you need a 5 lb supply of low-hydrogen electrodes for clean carbon steel and have a compatible AC or DCEP welder. Its smaller diameter offers useful puddle control, but moisture-sensitive storage, surface preparation, and correct procedures are essential. Choose a different electrode or process if you mainly weld dirty material, very thin sheet metal, or work that does not call for E7018.
Ready to Buy?
Check the current price, 3/32-inch size, and 5 lb package details before placing your order.